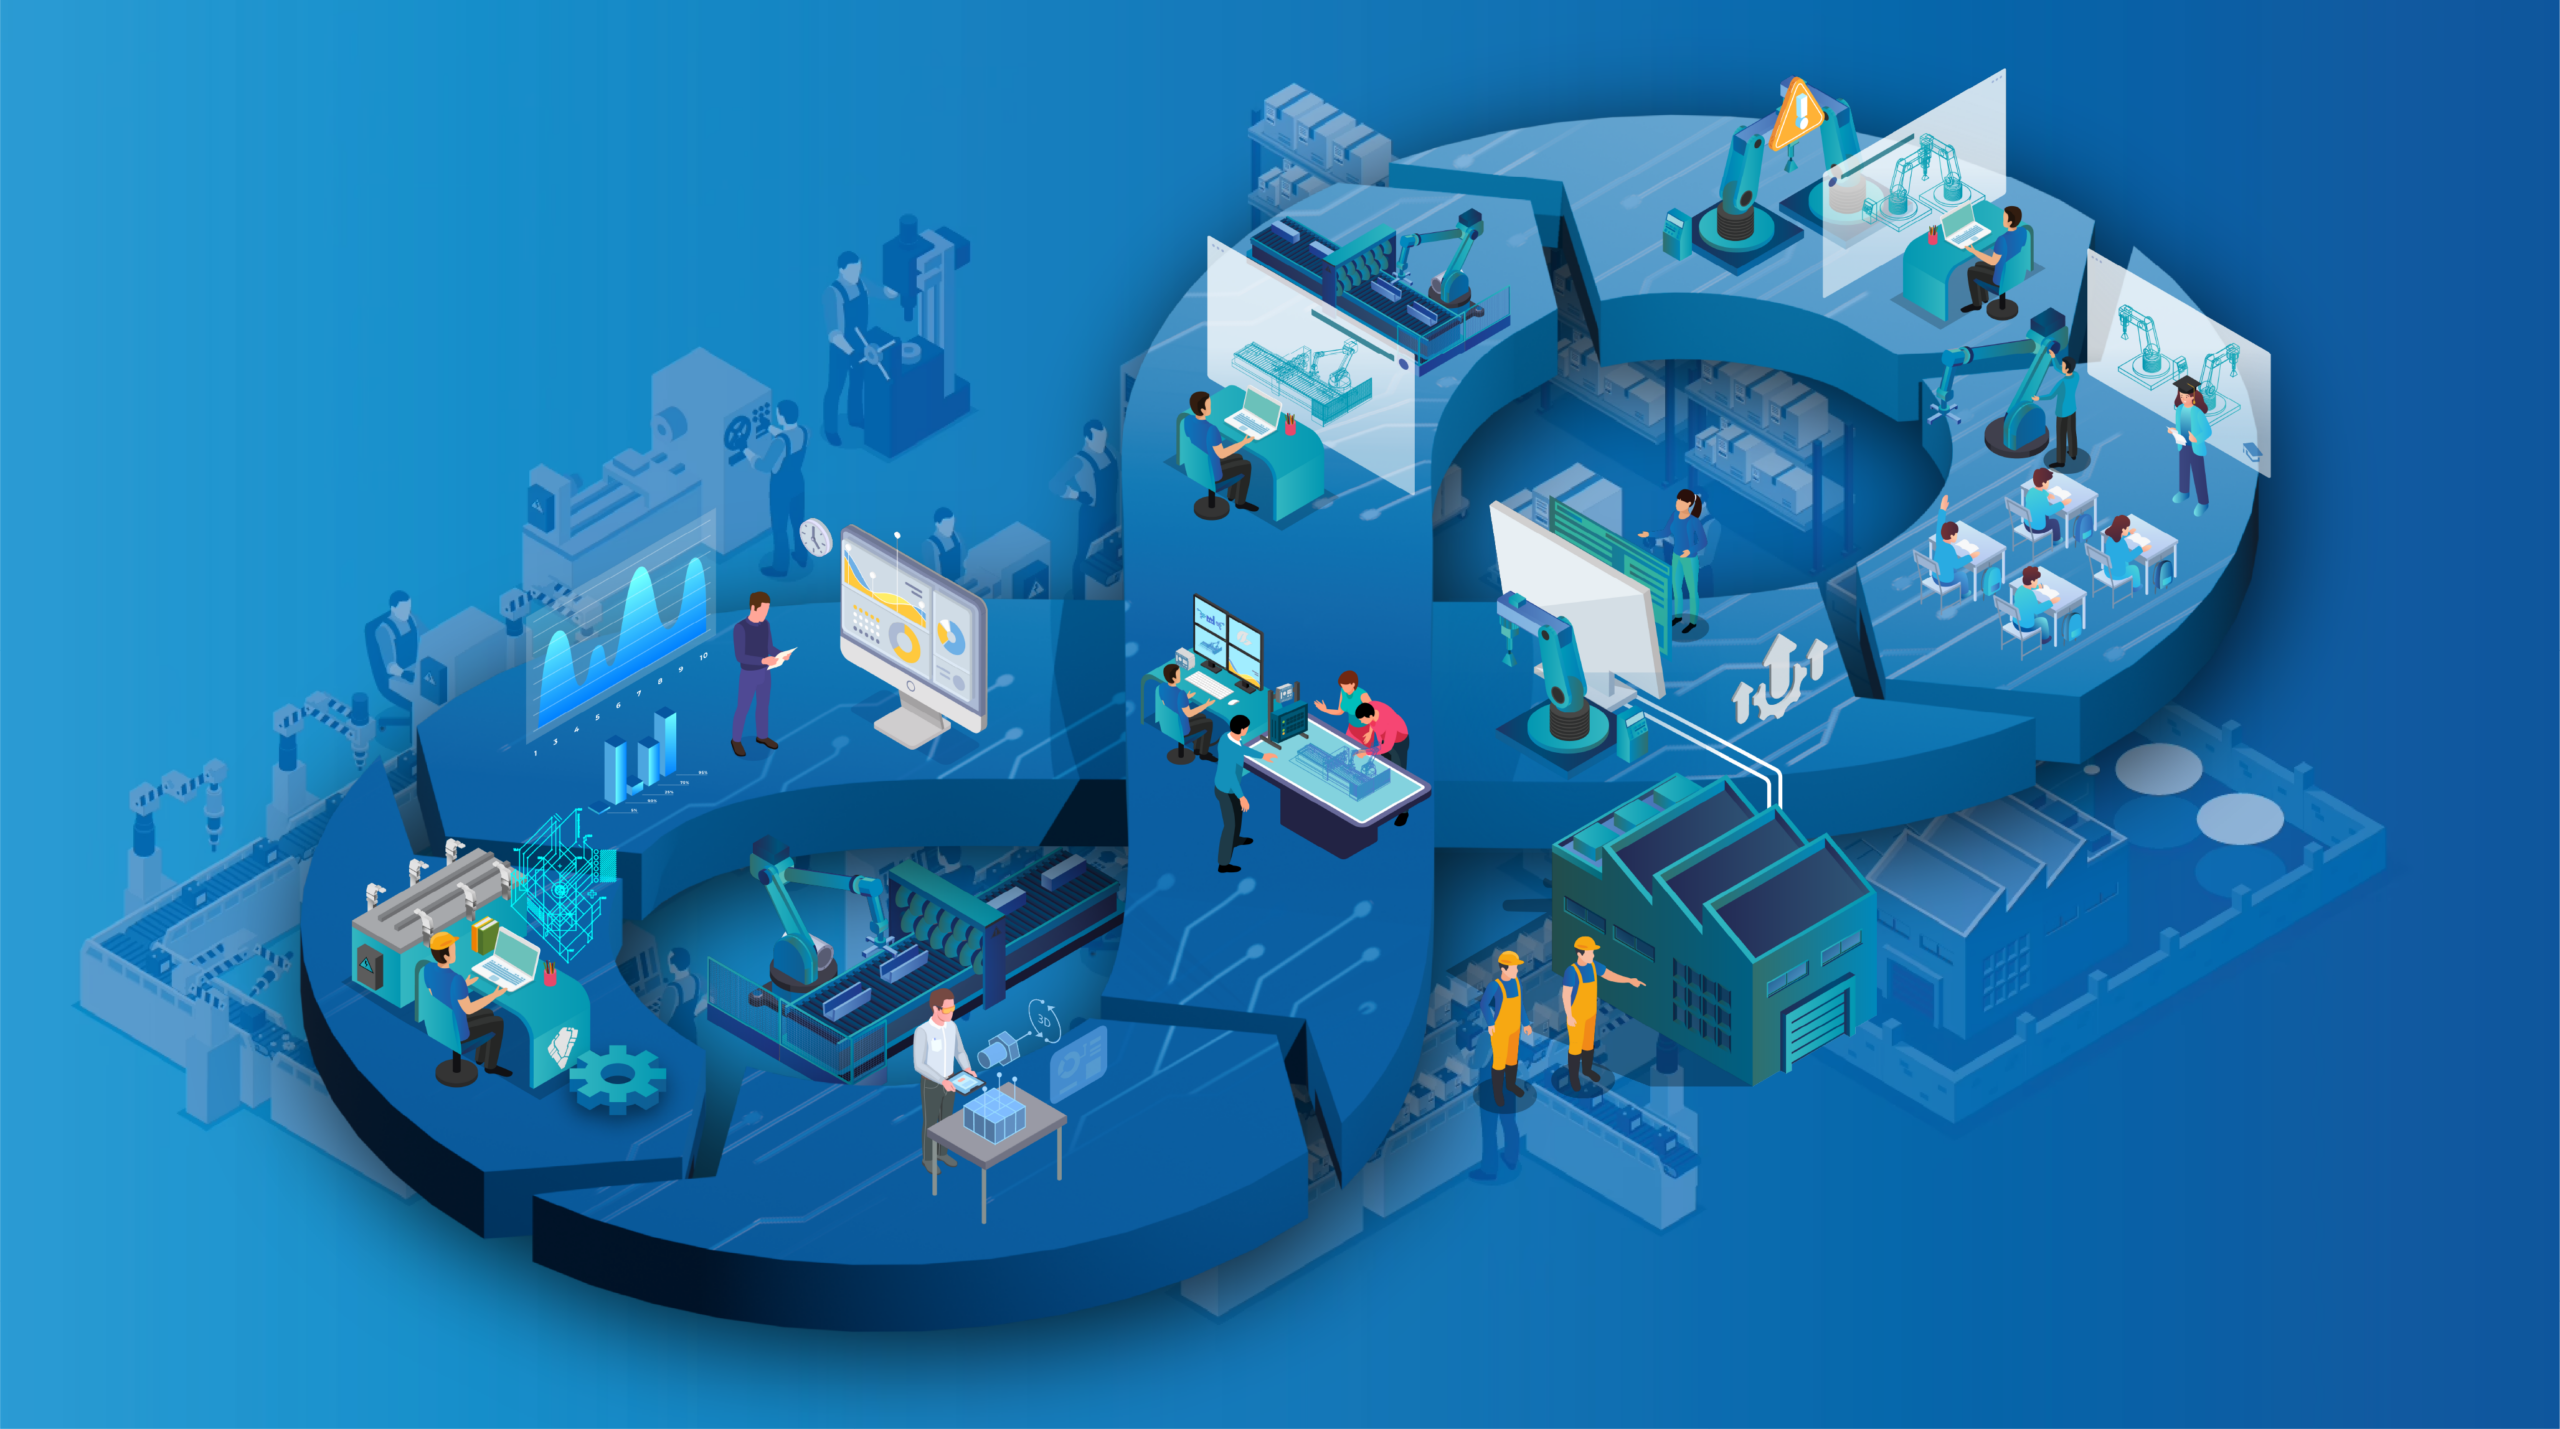
Entdecke alle Phasen der Automatisierung mit einem einheitlichen Ansatz.
Entdecke bewährte Anwendungsfälle für Tests, Validierung und Produktionsoptimierung.
Von der ersten Planung bis zu produktionsreifen Anlagen und automatisierten Engineering-Prozessen.
Entwickle zuverlässige Prozesse für die virtuelle Inbetriebnahme, industrielle Software und Wissen, das du immer wieder nutzen kannst.
Tools für die Digitale Fabrik
RF::SUITE
Eine vernetzte Plattform für Engineering, Simulation, Validierung und intelligenter Produktion.
RF::SUITE entdecken →
Wähle die passenden Werkzeuge für deinen Arbeitsablauf und verbinde sie in einer einheitlichen Engineering-Umgebung.
Von einzelnen Maschinen bis zu komplexen Produktionslinien: Wir verbinden Engineering, Simulation und Betrieb über den gesamten Lebenszyklus hinweg.
Industrien EntdeckenWir verbinden Simulation, virtuelle Inbetriebnahme und Know-how in industrieller Software für anspruchsvolle Produktionsumgebungen.
Wir beteiligen uns an nationalen und internationalen Forschungsprojekten zu digitalem Engineering, Automatisierung, künstlicher Intelligenz und nachhaltigen Produktionssystemen.
Resiliente, nachhaltige und anpassungsfähige industrielle Produktionssysteme.
→ 02 Forschungsprojekte REDRIVESResiliente Antriebstechnologien und robuste industrielle Produktionsprozesse.
→ 03 Forschungsprojekte DIGIKLEBDigitale Methoden für vernetzte Klebeprozesse und Qualitätskontrolle.
→ 04 Forschungsprojekte GENIUSIntelligente Ingenieurverfahren für datengetriebene Fertigungssysteme.
→Technologie und Erfahrung für zuverlässige industrielle Produktionssysteme.
Mehr über EKS InTec →Erfahre mehr über EKS InTec, unsere Standorte und deine Karrieremöglichkeiten – und nimm Kontakt mit unserem Team auf.
Digital Factory | Ramp-up
Ramp-up decides how quickly a new plant reaches its target output. We support this phase with engineering experience, the existing digital twin and RF::SUITE tools that make deviations visible, explainable and safe to correct.
The phase after start-up
During ramp-up, planned behavior meets real production: real parts, real tolerances, real operators and real disturbances. The work shifts from getting the system to move to understanding why it does not yet perform as intended — and correcting it without creating new risk.
Between the first produced part and stable series output, most losses come from timing, interlocks, material behavior and rare fault situations. These effects are only visible in operation — but they can be analysed, reproduced and corrected systematically instead of by trial and error on the running line.
What ramp-up really means
A plant that starts producing is not automatically a plant that produces at target rate. Waiting times, unexpected states, manual interventions and small recurring faults accumulate into availability losses that are hard to explain from the shop floor alone.
We approach ramp-up with the same data and models used during engineering and virtual commissioning, so real behavior can be compared with the intended behavior instead of being interpreted from memory.
Why structured ramp-up support pays off
The ramp-up phase is expensive: production is already scheduled, teams are on site and every unresolved effect repeats itself in every cycle. Structured analysis and simulation-based verification shorten this period and reduce the risk of quick fixes that cause new problems later.
Bottlenecks and waiting states are identified with data instead of assumptions.
Recurring faults are traced back to their cause in logic, signals or process behavior.
Optimizations are tested against the twin before they are loaded into the plant.
Operators and maintenance teams learn the system behavior in a controlled environment.
How we work during ramp-up
Target output, acceptance criteria, critical stations and the measures already taken are recorded so support starts from a shared picture.
Signal states, cycle times, fault messages and interlock conditions are recorded from the running system and prepared for structured evaluation.
Waiting states, blocking conditions, timing relationships and repeated faults are evaluated to separate symptoms from actual causes.
The simulation model is updated to the as-built system so the observed behavior can be reproduced offline and examined without stopping production.
PLC changes, robot programs and process parameters are tested against the model, including regression checks on functions that already worked.
Validated changes are transferred to the plant, documented with their test evidence and explained to the teams who operate and maintain the system.
Two ways through the ramp-up
Switch between a conventional ramp-up and a ramp-up supported by simulation and analysis to see how the working method changes — and where the time is won.
In a conventional ramp-up, corrections are made and verified on the running plant, so every iteration costs production time.
RF::SUITE during ramp-up
There is no separate ramp-up product. The value comes from continuing to use the models, connections and analysis functions that already exist from simulation and virtual commissioning — now applied to a plant that is actually producing.
Evaluates process sequences, cycle times, waiting states and interlocks so ramp-up losses can be located and quantified.
Explore RF::SCOUTKeeps the dynamic plant model available after start-up so observed behavior can be reproduced and optimizations tested offline.
Explore RF::YAMSProvides realistic device and signal behavior for retesting fault situations, sensor reactions and modified PLC logic.
Explore RF::ViPerSupports offline optimization of robot programs, handshakes and motion sequences while the cell continues to produce.
Explore RF::RobSimReconnects real controllers to the virtual environment so software changes can be validated with realistic signal exchange.
Explore RF::FSBoxKeeps model, signal and project data aligned with the as-built plant so the twin stays a reliable reference during ramp-up.
Explore RF::VPM ToolWhat we look at
Ramp-up problems rarely have a single cause. We work through the areas where planned behavior and real production most often drift apart, and document what was found, changed and verified.
Station times, transfer moments, synchronization and the stations that actually limit the line output.
Release conditions, handshakes and blocking situations that cost time without producing a visible fault.
Frequent messages, unclear diagnostics and error reactions that lead to manual intervention.
Path timing, waiting positions, collision avoidance and coordination with peripheral equipment.
Routing decisions, buffer filling, part tracking and the effect of variation in supply.
Behavior after stoppages, re-referencing, part handling and the time needed to return to automatic mode.
Setup functions, manual interventions and the operator actions that production currently depends on.
Software versions, test evidence and a traceable record of what was modified during ramp-up.
The twin after start-up
Once a plant is producing, every experiment on the real system competes with output. The digital twin gives the team a place to reproduce a problem, try an alternative sequence and check side effects without touching the running line.
RF::YAMS keeps the dynamic model usable after commissioning, so ramp-up optimization stays an engineering activity with verifiable results.
How EKS InTec supports you
Support during ramp-up can be a short analysis of one critical station or continuous engineering assistance until the line reaches its agreed output. The scope is defined together, based on the data available and the effects you are seeing.
Structured evaluation of cycle times, faults and waiting states to identify where the output is actually lost.
Automation engineers work with your team on control behavior, robot programs and integration issues during the ramp-up phase.
Software modifications and optimized sequences are tested against the model before they are released to the plant.
The simulation model is aligned with the delivered plant so it remains a valid reference for later changes.
Operators, maintenance and automation staff learn plant behavior and RF::SUITE methods in a risk-free environment.
Findings from ramp-up flow back into libraries, model standards and test scenarios for the next plant.
Prepare the phase in advance
Most of what makes ramp-up efficient is decided earlier: how much was validated virtually, whether the model stays maintained, which data is accessible and how changes are controlled once production has started.
Virtual commissioning is the strongest lever, because every function verified before start-up is one less thing to investigate on a running line.
Where ramp-up support helps most
Optimize handshakes, waiting positions and cell timing once real parts and real tolerances are involved.
Find the stations that limit line output and verify station-level changes without stopping the whole line.
Stabilize new equipment inside an existing plant where interference with running production is critical.
Improve routing, buffer behavior and transfer logic under real, variable material supply.
Refine control behavior and process parameters during the first production series at the customer site.
Analyse dependencies between machines, controls and robot systems that only appear in continuous operation.
Lifecycle view
The model created for planning and virtual commissioning does not lose its value at start of production. Kept up to date, it supports ramp-up, later software changes, training and the comparison between planned and real production behavior.
The same environment carries the plant through its lifecycle, which is what makes fast, verifiable reactions possible during ramp-up.
Continue exploring
Validate PLC logic, robot programs and system behavior before the plant exists to shorten the ramp-up that follows.
Explore virtual commissioningUse production data to understand system behavior, evaluate performance and keep improving after ramp-up.
Explore monitoringEnable your engineers to maintain models, run analyses and verify changes independently in future projects.
Explore software trainingFrequently asked questions
Your ramp-up phase
Whether your plant is about to start production or already fighting recurring losses, our team can help you analyse the behavior, verify the corrections and keep the digital twin useful for everything that follows.